Hits: 169 img
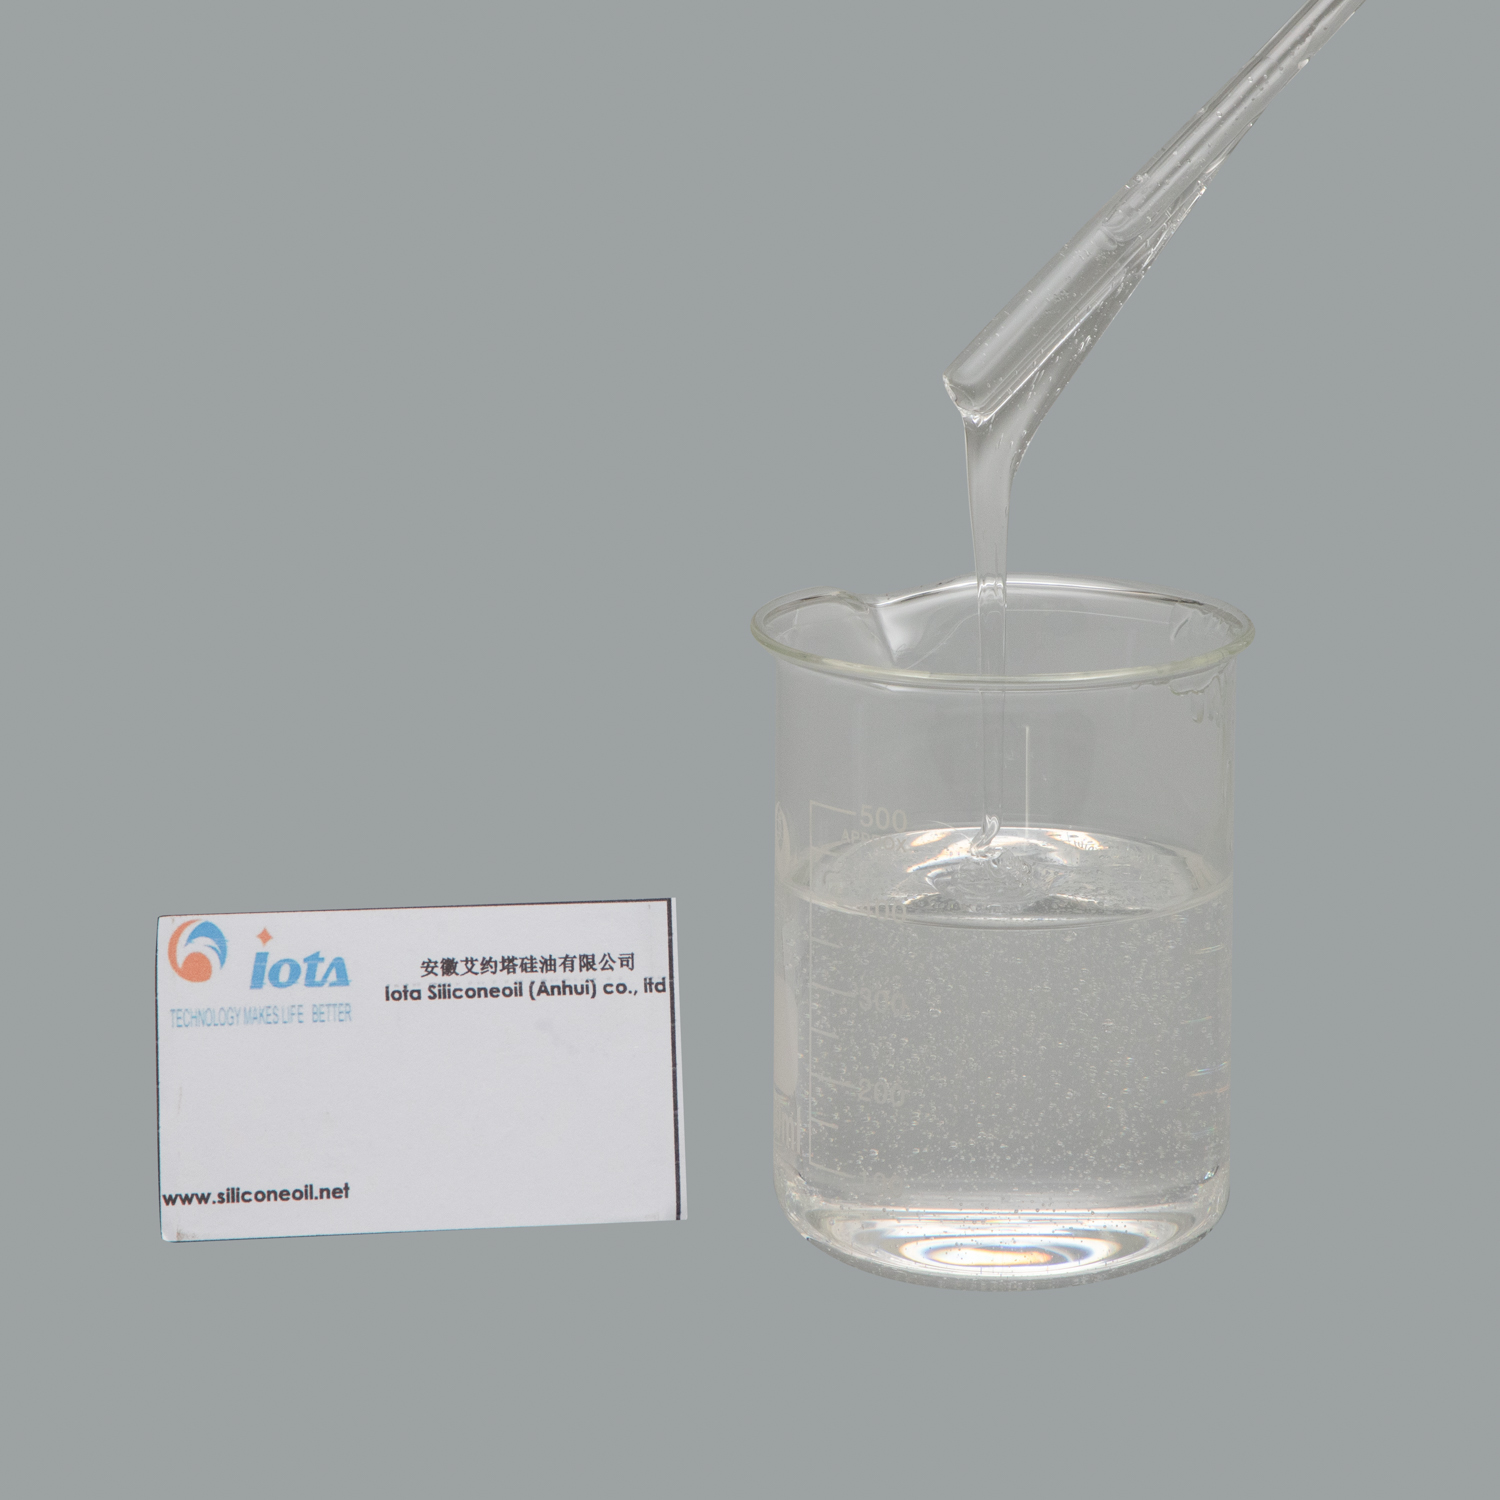
Against the ongoing global industrial trend that pushes advanced manufacturing systems toward more extreme operating conditions, methyl phenyl silicone oil — the specialty silicone polymer that uniquely combines exceptional high-low temperature resistance, radiation stability, electrical insulation and lubrication performance — is rapidly evolving from a little-known niche auxiliary chemical into a critical foundational material supporting the reliable operation of aerospace, nuclear power, ultra-high voltage power transmission and precision optical engineering sectors. Verified industry monitoring data shows that the global methyl phenyl silicone oil market exceeded 3.8 billion RMB in total value in 2025, with demand for high-phenyl-content specialty grades designed exclusively for extreme working scenarios registering an 11.3% year-on-year growth rate. This figure significantly outpaces the 3.7% average growth rate of conventional dimethyl silicone oil, marking a clear structural shift that has lifted the entire industry out of the old development model driven simply by general-purpose capacity expansion, and ushered in a new era defined by performance grading, scenario segmentation and custom formulation development.
Methyl phenyl silicone oil, CAS number 63148-58-3, is fundamentally a modified polydimethylsiloxane polymer where phenyl side groups are deliberately introduced along the siloxane backbone. The mass fraction of these phenyl substituents directly defines the material’s ultimate performance boundaries. Unlike conventional dimethyl silicone oil whose market growth is driven by simple downstream consumer demand expansion, the rising adoption of methyl phenyl silicone oil is fueled by the underlying technical requirements of high-end equipment industries that continuously push the limits of temperature, radiation and electrical stress. Over the past five years, more than 72% of new-generation equipment design projects in aerospace engine hot-section lubrication systems, nuclear reactor main pump damping media and UHV bushing insulating filling fluids have explicitly specified methyl phenyl silicone oil as the core functional medium, up from less than 30% in 2020. This statistic clearly demonstrates that the material is no longer treated as an optional alternative, but has become an irreplaceable component of many critical industrial systems.
Today’s global methyl phenyl silicone oil industrial landscape presents a distinct dual structure: general-purpose low-phenyl grades are produced in large volumes with abundant market supply, while high-purity, high-performance specialty grades for aerospace, nuclear and long-lifetime high-reliability applications remain highly concentrated among manufacturers that have mastered complete full-process quality control capabilities. This structural supply-demand difference is systematically pushing the entire industry away from the old competition model that prioritized output scale, and toward a new technical competition stage centered on precise molecular structure regulation, multi-year extreme-condition reliability validation and full-lifecycle quality traceability.
The performance differences between various methyl phenyl silicone oil products originate fundamentally from the proportion of phenyl groups introduced into the polydimethylsiloxane molecular chain. The industry formally categorizes all commercial products into three distinct technical tiers: low-phenyl type (5%~12% phenyl content), medium-phenyl type (12%~30% phenyl content) and high-phenyl type (30%~45% phenyl content). Products in different tiers exhibit significant divergence in molecular chain configuration, microscopic aggregation state structure and macroscopic service performance, corresponding to completely different application scenario boundaries.
Low-phenyl methyl phenyl silicone oil represents the earliest category to achieve large-scale industrialization. With relatively low phenyl substitution ratios along the molecular backbone, this product class retains the excellent low-temperature resistance of conventional dimethyl silicone oil while moderately improving high-temperature tolerance and radiation resistance. Its freezing point typically drops below -45°C, with specially customized formulations reaching as low as -60°C. At the same time, the maximum long-term service temperature is elevated from 180°C for regular dimethyl silicone oil to 220°C, and the viscosity-temperature coefficient is controlled below 0.6, ensuring minimal viscosity variation across an extremely wide temperature range. These characteristics make low-phenyl grades the most widely used and highest-volume product category, deployed in damping fluids for outdoor equipment operating in extremely cold regions, low-temperature condition bearing lubricants and pressure transmission media for precision instruments and meters.
Medium-phenyl methyl phenyl silicone oil represents the mainstream technical level for current industrial-grade applications, with phenyl mass fraction precisely controlled between 12% and 30%. This performance tier delivers step-change improvements in thermal stability, radiation resistance and electrical insulation properties. The long-term continuous service temperature reaches 250°C, while short-term peak temperature tolerance can exceed 330°C. Open flash points are universally maintained above 300°C, with some high-flash-point formulations reaching 320°C or higher. In addition, medium-phenyl grades demonstrate far superior corona resistance, ozone aging resistance and shear stability compared to standard dimethyl silicone oil, with breakdown voltage strength consistently stabilizing above 15kV/mm. These properties have made medium-phenyl methyl phenyl silicone oil the material of choice for electrical insulation, high-temperature hydraulic systems and vacuum diffusion pump oil applications. The core technical challenge for this product class lies in ensuring uniform distribution of phenyl groups along the entire molecular chain, avoiding local phenyl enrichment or segmented block structures that would otherwise cause abnormal viscosity increase and performance degradation during long-term high-temperature service.
High-phenyl methyl phenyl silicone oil belongs to the strategic specialty material category developed exclusively for extreme special operating conditions, with phenyl mass fraction reaching 30%~45%. Some aerospace-grade custom formulations can further elevate phenyl content to even higher levels. The extremely high phenyl density along the molecular backbone delivers exceptional resistance to high-energy radiation and high-temperature oxidative stability. After exposure to cumulative gamma radiation doses exceeding 10⁶Gy, the material still retains basic fluidity and insulating properties, without undergoing obvious molecular chain scission or cross-linking solidification that would completely degrade most conventional organic materials. These products are irreplaceable core working media for nuclear power primary loop auxiliary systems, deep-space exploration spacecraft external operating environments and special electrical equipment operating at high altitudes under intense radiation conditions. They also represent the highest point of global technical competition in the methyl phenyl silicone oil industry today.
The industrial manufacturing of methyl phenyl silicone oil is far more complex than simple monomer mixing and polymerization. It represents a complete and sophisticated production chain covering monomer purification, co-hydrolysis, equilibrium polymerization, low-molecular component removal and post-treatment refining. Insufficient control precision at any single stage will directly prevent the final product from meeting the long-term reliability requirements of high-end application scenarios. While the mainstream mature industrial production route universally adopts the co-hydrolysis polycondensation technology path using methyl chlorosilane and phenyl chlorosilane, products from different manufacturing systems show dramatic differences in key indicators such as molecular weight distribution, residual low-molecular content and trace metallic ion impurity levels. This fundamental reality explains why high-performance specialty grades cannot be easily replicated through simple imitation.
The raw material refining stage forms the first critical checkpoint determining the final product grade. Raw monomers including dimethyldichlorosilane, methylphenyldichlorosilane and hexamethyldisiloxane must undergo multi-column continuous distillation purification to elevate monomer purity above 99.9%, while strictly controlling trace water, free acid and other impurity monomer contents. If excessive trifunctional impurities are accidentally introduced into the phenyl chlorosilane monomer, they will generate localized branching and micro-gel structures during the polymerization process, eventually leading to insoluble particle precipitation during long-term high-temperature operation that directly compromises the reliability of lubrication or insulation systems. In high-grade production systems, every batch of monomers passes through online real-time spectral inspection before entering the reaction stage, ensuring that monomer composition perfectly matches the formulation design requirements.
The co-hydrolysis and equilibrium polymerization stage forms the absolute core of the entire production process. In traditional process workflows, mixed methyl chlorosilane and phenyl chlorosilane monomers are slowly added dropwise to excess water under strictly temperature-controlled conditions. This highly exothermic reaction must be maintained steadily between 30°C and 50°C through precise jacket cooling systems, preventing local overheating that would otherwise cause phenyl group hydrolysis and detachment. After hydrolysis is completed, the resulting silanol intermediate undergoes multiple neutralization and water washing cycles to remove residual hydrogen chloride and salt byproducts, before being transferred to the polymerization reactor. Under the catalysis of selected alkaline or acidic catalysts, the system undergoes high-temperature vacuum equilibrium polymerization, where hexamethyldisiloxane acts as a blocking agent to precisely control the final molecular weight and viscosity distribution. For high-performance specialty grades, the equilibrium polymerization reaction typically continues for dozens of consecutive hours with continuous online viscosity monitoring, ensuring the polymer molecular weight distribution index is controlled below 1.2, far superior to the 1.6~1.8 range commonly seen in general-purpose industrial products.
The low-molecular removal and post-treatment refining stage represents the critical watershed that separates ordinary industrial-grade products from premium specialty grades. The crude product obtained after equilibrium polymerization still contains significant quantities of low-boiling cyclic siloxane monomers and incompletely polymerized low-molecular linear siloxane components. If residual content of these components remains too high, the final product will exhibit severe thermal weight loss and volatile loss during high-temperature operation, directly undermining the long-term operational stability of the entire system. High-performance grades universally adopt multi-stage high-vacuum thin-film evaporation processes, which completely remove low-molecular components at temperatures far below the material’s thermal decomposition point. The final finished product typically demonstrates less than 0.5% mass loss after 2 hours of thermal testing at 250°C, far exceeding the 3%~5% performance level common for general-purpose products. Subsequent activated carbon adsorption, precision filtration and ion exchange treatments further reduce trace metallic ion impurity content to ppb levels, fully meeting the ultra-high purity requirements of nuclear power and semiconductor-grade applications.
For decades, methyl phenyl silicone oil was treated as an ordinary auxiliary lubricant in industrial systems, and its true value remained chronically underestimated. However, as modern high-end equipment systems continuously push their operating environments toward higher temperature, stronger radiation and wider temperature ranges, the irreplaceability of methyl phenyl silicone oil as a core working medium is rapidly emerging. A large number of extreme-condition equipment design solutions that were previously technically impossible can only be realized today thanks to performance breakthroughs in methyl phenyl silicone oil technology.
In the ultra-high voltage power transmission sector, methyl phenyl silicone oil serves as the core insulating filling medium inside high-voltage bushings and power capacitors. Traditional mineral insulating oil easily undergoes aging decomposition under long-term high temperature and strong electric field conditions, generating flammable gases that create severe safety hazards. Methyl phenyl silicone oil not only delivers excellent electrical insulation performance with flash points far higher than mineral oil, but also possesses natural corona resistance and partial discharge tolerance. Even under prolonged exposure to high electric field strength, it does not generate large quantities of carbonaceous deposits that degrade insulation performance, significantly extending the operational lifetime of UHV equipment. Today, multiple large-scale UHV AC transmission projects have widely adopted methyl phenyl silicone oil as their core insulating filling medium, achieving dramatic improvements in overall system operational reliability.
In the aerospace sector, methyl phenyl silicone oil functions as the critical working fluid for high-temperature bearing lubrication, damping and shock absorption systems and thermal control systems. The onboard equipment of some long-endurance high-altitude aircraft must operate continuously and stably across the ultra-wide temperature range from -55°C to 200°C. Conventional lubricating oils completely solidify at low temperatures and oxidize and fail at high temperatures, making them completely unsuitable for these extreme requirements. Specially refined high-purity methyl phenyl silicone oil, with its extremely low freezing point, exceptional thermo-oxidative stability and extraordinarily wide liquid temperature range, has become the only technically feasible lubrication and damping medium for these scenarios, ensuring that onboard inertial navigation platforms maintain extremely high operational accuracy across the entire flight envelope.
In the nuclear power industry, methyl phenyl silicone oil acts as the critical reliability guarantee material for reactor main pump dampers and related auxiliary systems. The intense radiation environment inside nuclear power facilities causes molecular chain degradation in the vast majority of organic materials, eventually making them lose their original functional properties. Specially formulated high-phenyl-content methyl phenyl silicone oil, after prolonged exposure to neutron and gamma radiation, still maintains excellent fluidity and damping performance without obvious solidification or viscosity increase. It has become an irreplaceable functional material in the nuclear power safety operation system. Beyond these flagship sectors, methyl phenyl silicone oil also plays an irreplaceable role in numerous other high-end niche scenarios including vacuum diffusion pump oil, high-temperature mold release agents and precision optical instrument damping fluids, quietly operating as the “invisible cornerstone” that supports the stable operation of the entire advanced manufacturing ecosystem.
The global methyl phenyl silicone oil industry is currently facing an unprecedented strategic development opportunity window. On one hand, the ongoing global advanced manufacturing upgrading wave continues to pull market demand for high-performance methyl phenyl silicone oil, and application scenarios that previously relied entirely on imported specialty grades are now accelerating domestic material validation and substitution processes. On the other hand, advances in molecular design technology and continuous production process innovation are continuously pushing methyl phenyl silicone oil beyond its traditional performance boundaries, opening up entirely new application scenarios that were unimaginable in the past.
Over the next three to five years, the industry’s technical development roadmap will focus on three core dimensions. First, further improving batch stability and mass production scale of high-phenyl specialty grades, significantly reducing manufacturing costs for premium products and making stable and reliable material supply accessible to more extreme-condition scenarios. Second, developing composite modified products that combine the fundamental performance of methyl phenyl silicone oil with additional targeted functionalities through further side-group modification, such as introducing reactive groups to achieve in-situ curing at high temperatures or adding specific elements to further enhance radiation resistance, thereby expanding the material’s overall performance envelope. Third, establishing a complete extreme-condition long-term reliability database covering the entire material lifecycle, providing full sets of material performance data for the design of long-lifetime equipment in aerospace and nuclear power sectors, and completely closing the critical material data gap that currently constrains advanced equipment design.
As methyl phenyl silicone oil’s industrial technology system continues to mature, this specialty silicone material that has long remained hidden behind industrial equipment will play an even more central enabling role in more extreme scenarios that were previously inaccessible, becoming the key material foundation that supports the next generation of advanced manufacturing systems as they push into deeper, farther and more extreme operating conditions.